Polyester blend fabric is one of the most widely used materials in bag manufacturing — yet it’s also one of the most misunderstood. Ask a supplier for “polyester blend” and you’ll get a dozen different answers, because the term covers a broad range of fiber combinations, each with different performance profiles.
For brands and procurement teams sourcing custom bags, understanding what polyester blend actually means — and how blend ratio affects print quality, durability, water resistance, and cost — is the difference between a product that performs and one that disappoints.
This guide covers everything you need to know: what polyester blend fabric is, the most common types used in bag production, how different blends behave under real-world conditions, and how to specify the right material when placing a bulk order.
What Does “Polyester Blend” Mean?
Polyester blend fabric is any textile made by combining polyester fibers with one or more other fibers — natural or synthetic. The result is a material that inherits performance characteristics from each component.
Polyester itself is a synthetic fiber derived from petroleum-based polymers. It is valued in bag manufacturing for its durability, wrinkle resistance, dimensional stability, and relatively low cost. Its primary weaknesses are lower breathability, a synthetic hand feel, and limited compatibility with certain printing methods.
Blending polyester with another fiber — cotton, nylon, spandex, linen, or recycled alternatives — allows manufacturers to offset these weaknesses while preserving polyester’s structural advantages.
Blend ratio is the critical variable. A label reading “65% Polyester / 35% Cotton” means 65 parts polyester fiber to 35 parts cotton, by weight. Common ratios include:
| Ratio | Polyester Dominant? | Typical Use Case |
|---|---|---|
| 80/20 (Poly/Cotton) | Yes | Promotional bags, budget totes |
| 65/35 (Poly/Cotton) | Yes | General-purpose bags, uniforms |
| 50/50 (Poly/Cotton) | Equal | Retail totes, print-forward products |
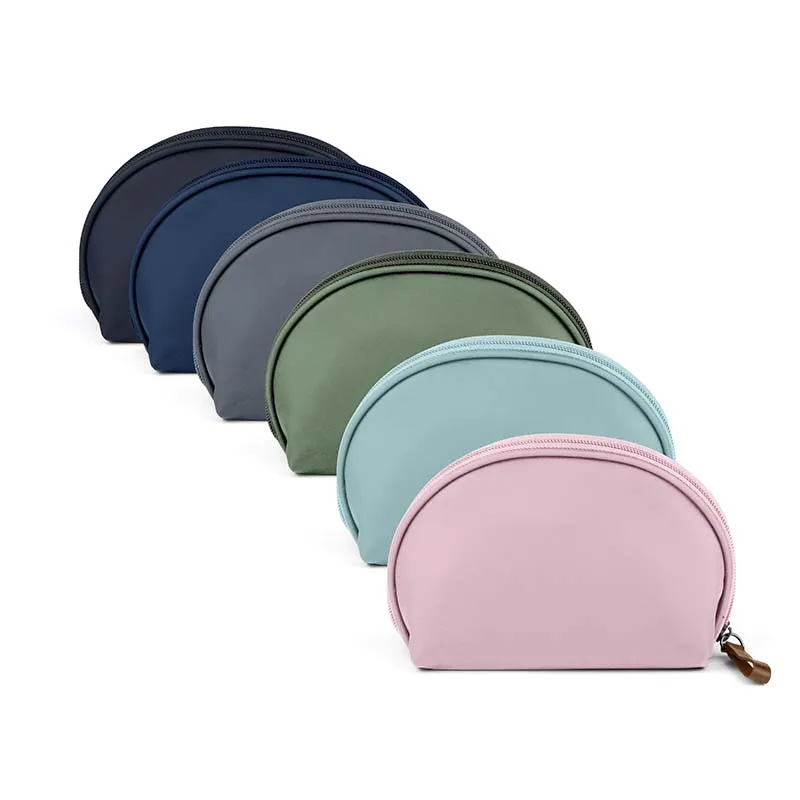
| 70/30 (Poly/Nylon) | Yes | Travel bags, cosmetic bags |
| 90/10 (Poly/Spandex) | Yes | Fitted pouches, elastic linings |
The ratio is not just a label — it directly determines how the fabric performs across durability, printability, water resistance, and cost. More on this below.
How Polyester Blend Fabric Is Made
Understanding the manufacturing process helps explain why two fabrics with the same labeled ratio can feel and perform differently.
Fiber-level blending is the most common method. Polyester and cotton (or other) staple fibers are mixed before being spun into yarn. This produces a uniform fabric where both fibers are evenly distributed throughout. Most bag fabrics — 210D polycotton, promotional tote fabrics — are made this way.
Yarn-level blending combines separately spun yarns during weaving or knitting. This can produce textured or two-tone effects, and is sometimes used in fashion-forward bag fabrics or structured canvas alternatives.
After spinning and weaving, finishing treatments are applied depending on the end use:
- PU coating — the standard for water resistance in bag fabrics; applied to one side
- PVC coating — heavier, fully waterproof, used for industrial or heavy-duty applications
- Anti-wrinkle treatment — common in higher cotton-content blends
- Printing preparation — surface treatments that affect ink adhesion for screen printing or digital methods
The finishing stage is where bag fabrics diverge most from apparel blends. A polycotton tote fabric and a polycotton T-shirt fabric may share the same fiber ratio but be finished entirely differently for their respective applications.
The 5 Most Common Polyester Blends Used in Bags
Polyester / Cotton (Polycotton)
The most widely used blend in bag manufacturing. Cotton improves hand feel, breathability, and compatibility with screen printing and heat transfer. Polyester provides structure, reduces shrinkage, and speeds drying time.
Common ratios: 65/35, 80/20, 50/50
Typical GSM range: 150–280 GSM
Best for: Promotional tote bags, gift bags, branded merchandise bags, shopping bags
Print methods: Screen printing, heat transfer, DTG (high cotton content)
Polyester / Nylon
Nylon adds abrasion resistance and tensile strength beyond what polyester alone provides. This blend is common in bags that need to handle repetitive stress — zippers, straps, and corners that take the most wear.
Common ratios: 70/30, 60/40
Best for: Travel bags, cosmetic bags, toiletry pouches, laptop sleeves
ملاحظة: Nylon content increases cost; specify only where durability demands it
Polyester / Spandex (Elastane)
A small percentage of spandex (typically 5–10%) adds stretch and recovery without significantly changing the fabric’s appearance. Common in form-fitting pouches and bag linings where a snug fit matters.
Common ratios: 90/10, 95/5
Best for: Cosmetic pouches, organizer inserts, elasticated bag linings
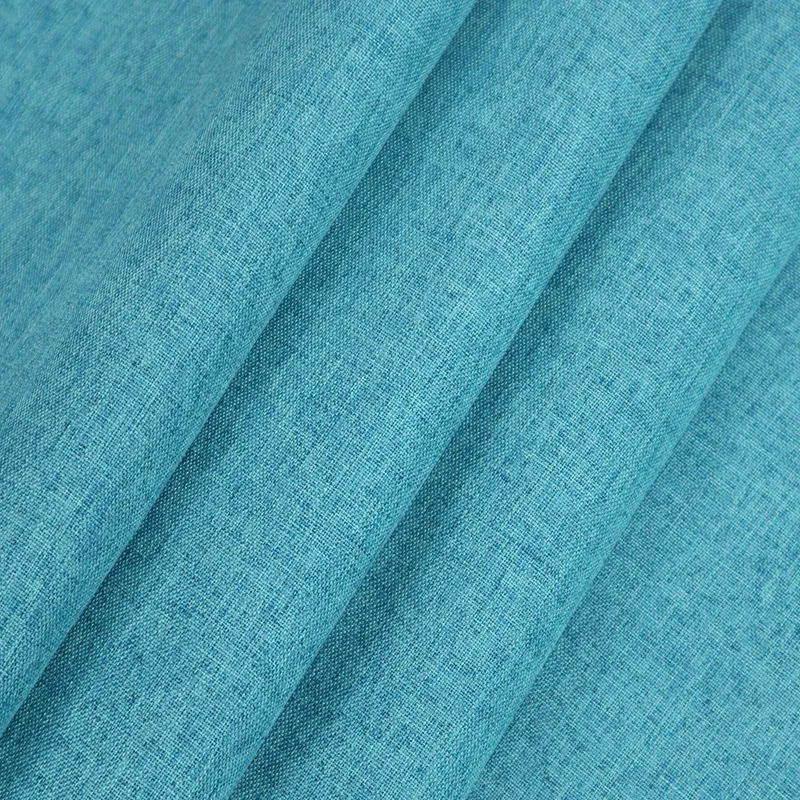
Polyester / Linen
Linen adds a natural texture and visual warmth that reads as more premium than pure synthetic fabric. The polyester component reduces linen’s tendency to crease severely and improves dimensional stability.
Common ratios: 55/45, 60/40
Best for: Retail tote bags, beach bags, fashion-forward branded bags, summer collections
Consideration: Higher linen content raises cost and limits some coating options
rPET / Cotton or rPET / Linen
Recycled polyester (rPET) made from post-consumer plastic bottles can be blended with cotton or linen to combine sustainability credentials with improved hand feel. This is an increasingly common choice for brands making environmental claims.
Certifications available: Global Recycled Standard (GRS), Recycled Claim Standard (RCS)
Best for: Eco-branded promotional bags, retail collections with sustainability positioning
How Blend Ratio Affects Bag Performance
This is where most generic fabric guides fall short. For bag buyers, four performance variables shift meaningfully as blend ratio changes.
1. Water Resistance
Cotton absorbs moisture; polyester repels it. As cotton content increases, the fabric’s inherent water resistance decreases — meaning a higher reliance on PU or PVC coating to achieve the same performance target.
A 65/35 polycotton bag fabric with PU coating will perform adequately for light rain. A 100% polyester fabric with the same coating will perform better under sustained exposure. If water resistance is a primary requirement, keep cotton content at or below 35%, or compensate with a heavier coating specification.
2. Print Compatibility
This is the most practically significant variable for branded bag buyers:
| Blend | Screen Printing | Heat Transfer | Sublimation | DTG |
|---|---|---|---|---|
| High cotton (≥50%) | Excellent | Good | Not suitable | Good |
| Balanced (65/35) | Good | Good | Poor | Moderate |
| High polyester (≥80%) | Moderate | Moderate | Excellent | Poor |
| 100% Polyester | Moderate | Moderate | Best | Not suitable |
Key implication: If your design requires full-coverage, photographic-quality all-over printing, you need high polyester content for sublimation. If you need sharp, opaque logo printing with screen or heat transfer, higher cotton content produces better adhesion and color saturation. Always confirm your chosen print method before finalizing fabric specification.
3. Structural Weight (GSM)
GSM (grams per square meter) and blend ratio are related but independent variables. A 200 GSM polycotton fabric and a 200 GSM pure polyester fabric will feel different — the polycotton typically has a softer, more substantial hand feel, while the polyester feels lighter and more technical.
For reference, common bag fabric weight ranges:
- 150–180 GSM — lightweight promotional bags, foldable totes
- 200–250 GSM — standard retail and branded bags
- 260–300 GSM — heavy-duty shopping bags, structured bags
4. Cost
As a general rule, higher cotton content increases raw material cost. However, a high-cotton blend may reduce finishing costs if it eliminates the need for certain coatings. The total cost calculation should include fabric, finishing treatment, and any printing method implications.
Polyester Blend vs 100% Polyester: Which Is Better for Bags?
Neither is universally better. The right choice depends on end use, print method, and brand positioning.
| Decision Factor | Choose Polyester Blend | Choose 100% Polyester |
|---|---|---|
| Primary print method | Screen print, heat transfer | Sublimation |
| Water resistance priority | Low to medium | عالية |
| Brand positioning | Premium, soft-touch feel | Functional, promotional |
| Coating required? | Often optional | Usually required |
| Sustainability claim (rPET) | Available | Also available |
| Cost sensitivity | Moderate | Lower |
A polycotton blend is typically the better choice for promotional bags and branded totes where print clarity and perceived quality matter. Pure polyester is more appropriate for bags where water resistance, sublimation printing, or cost minimization is the primary driver.
Printing on Polyester Blend Fabrics: What Bag Buyers Need to Know
Print method and fabric composition must be matched at the sourcing stage — not after samples arrive.
الطباعة بالشاشة works best on cotton-rich blends (50% cotton or higher). The ink bonds well to natural fibers and produces sharp, opaque results. It is the standard method for logo-forward promotional bags.
Heat transfer / heat press is compatible with most polycotton blends. Works reliably on 65/35 and higher cotton ratios. Less suitable for high-polyester fabrics where adhesion can degrade over time.
Sublimation printing requires a minimum of 80% polyester content — typically 100% polyester for best results. It produces vivid, full-color, edge-to-edge prints that are embedded in the fiber (not sitting on top). Cannot be used on cotton-dominant blends; colors will appear faded and washed out.
Embroidery is compatible with most woven polycotton blends. Higher GSM fabrics provide better backing stability. Confirm with your supplier that the fabric weight is sufficient to support the stitch count without puckering.
Practical tip for buyers: When briefing a factory, state your intended print method before asking them to recommend fabric. A good manufacturer will reverse-engineer the fabric specification from the print requirement, not the other way around.
Sustainability Options: rPET Blends and Certifications
Polyester’s primary sustainability liability is its petroleum origin and non-biodegradable end-of-life profile. Two approaches are used to address this in B2B bag sourcing:
Recycled Polyester (rPET): Produced from post-consumer plastic bottles or post-industrial polyester waste. Functionally near-identical to virgin polyester in most bag applications. Can be blended with cotton or linen to improve hand feel.
Key certifications for rPET blend fabrics:
- Global Recycled Standard (GRS) — certifies recycled content claim and chain of custody. Most widely recognized for B2B and retail claims.
- Recycled Claim Standard (RCS) — narrower scope, covers recycled content only without the full supply chain requirements of GRS.
- OEKO-TEX Standard 100 — certifies absence of harmful substances. Applies to both virgin and recycled polyester blends. Does not verify recycled content claims.
Important limitation: GOTS (Global Organic Textile Standard) requires 100% certified organic fiber. A polyester/organic cotton blend cannot carry GOTS certification. If organic credentials are important to your brand, confirm the certification pathway with your supplier before committing to a blend specification.
Sourcing tip: Always request the actual certification document, not just a supplier’s verbal claim. GRS certificates are issued per production facility and have expiration dates — verify they are current.
How to Specify Polyester Blend Fabric When Ordering Custom Bags
Vague fabric briefs are one of the most common causes of quality issues in custom bag production. Suppliers who receive “polyester blend” as a specification will substitute whatever is cost-effective — which may not match your requirements.
A complete fabric specification should include:
- Fiber composition and ratio — e.g.,
65% Polyester / 35% Cotton - Fabric weight — e.g.,
210 GSM - Construction type — e.g.,
plain weaveأوripstop - Finishing treatment — e.g.,
single-side PU coatingأوuncoated - Certifications required — e.g.,
GRS certified rPETأوOEKO-TEX 100
Example spec: 65% Polyester / 35% Cotton, 220 GSM, plain weave, uncoated, OEKO-TEX 100 certified
Common sourcing pitfalls to avoid:
- Unlabeled blend ratios: Some factories list fabric as “polycotton” without specifying the ratio. Always request a Fabric Test Report or material composition certificate for bulk orders.
- GSM substitution: Factories may substitute a lighter GSM fabric of the same blend if not explicitly specified. Include GSM tolerance in your purchase order (e.g., ±5%).
- Coating specification: “Water resistant” is not a specification. State the coating type and, for performance applications, the hydrostatic head rating required.
Sample confirmation checklist:
- [ ] Hand feel matches brief
- [ ] Weight verified against GSM spec (weigh a 10×10cm sample)
- [ ] Print test approved for your intended method
- [ ] Wash test completed (check for shrinkage and colorfastness)
- [ ] Certification documents received and verified
Is Polyester Blend Fabric Good for Bags?
Yes — for most bag categories, a polyester blend outperforms both pure polyester and pure natural fibers when the blend is correctly matched to the application.
Where polycotton blends perform well:
- Promotional tote bags and shopping bags (logo clarity, perceived quality, cost efficiency)
- Gift bags and retail packaging bags (hand feel, printability)
- Lightweight travel accessories (durability with comfort)
Where high-polyester or pure polyester performs better:
- Cooler bags and waterproof bags (coating adhesion, water resistance)
- Sublimation-printed bags (dye bonding requires polyester-dominant content)
- Budget promotional items where cost is the primary constraint
Where other blends have specific advantages:
- Poly/nylon for cosmetic bags and toiletry bags requiring high abrasion resistance
- Poly/linen for retail totes and beach bags where natural aesthetics are part of the brand story
- rPET blends for sustainability-positioned collections
Frequently Asked Questions
What does “polyester blend” mean on a bag label? It means the fabric is made from polyester combined with at least one other fiber. The label should also state the fiber composition ratio (e.g., 65% Polyester / 35% Cotton). If it doesn’t, request a material specification sheet from the supplier.
Is polyester blend fabric waterproof? Not inherently. Cotton-containing blends absorb moisture unless coated. Water resistance depends on the finishing treatment applied — PU coating provides splash resistance; PVC coating provides full waterproofing. The base fabric blend affects how well coatings adhere and perform over time.
Is polycotton good for custom printed bags? Yes — polycotton with 35–50% cotton content is one of the best substrates for screen printing and heat transfer. It produces sharper, more vibrant results than pure polyester for these methods. For sublimation printing, you need high polyester content (80%+).
What is the difference between polyester blend and 100% polyester? A polyester blend incorporates at least one other fiber, which typically improves hand feel, breathability, and compatibility with certain printing methods. 100% polyester is more water-resistant by nature, better suited to sublimation printing, and usually lower cost, but has a more synthetic feel and fewer print method options.
Can polyester blend fabric be recycled? Blended fabrics are generally more difficult to recycle than single-fiber fabrics because separating fiber types at end-of-life is technically challenging. If recyclability or circularity is important to your brand, consider using rPET-based blends (which reduce demand for virgin polyester at the input stage) and communicate clearly about end-of-life options to customers.
Which polyester blend is best for promotional bags? For most promotional bag applications — totes, drawstring bags, non-woven alternatives — a 65/35 or 80/20 polyester/cotton blend at 180–220 GSM provides the best balance of cost, print quality, and durability. For eco-positioned promotional bags, an rPET/cotton blend with GRS certification is the most credible option.
Summary: Choosing the Right Polyester Blend for Your Bag Project
Polyester blend fabric is not a single material — it is a category of materials that ranges from budget polycotton promotional fabric to performance rPET/nylon blends for technical travel bags. The right choice depends on four decisions made in sequence:
- What is the bag’s primary function? (promotional, retail, travel, waterproof)
- What is the intended print method? (sublimation → high polyester; screen/heat transfer → higher cotton)
- What is the water resistance requirement? (determines coating specification)
- What are the sustainability or certification requirements? (determines fiber sourcing)
Once those four variables are defined, fabric specification becomes straightforward — and your supplier can produce to a clear, verifiable brief.
Looking for custom bags made from polyester blend fabrics? Our team can help you select the right material, weight, print method, and construction for your project. اتصل بنا for samples and bulk pricing.
Related articles:

 Arabic
 English
 French
 German
 Japanese
 Thai
 Vietnamese
 Russian
 Spanish
 Portuguese